1
Delta Tau PMAC Software Reference V1.17
F
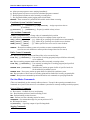
Function
Scope
Syntax
Remarks
Example
See Also
Report motor following error
Motor specific
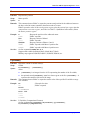
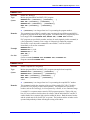
F
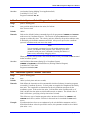
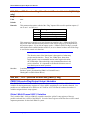
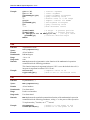
This command causes PMAC to report the present motor following error (in counts, rounded
to the nearest tenth of a count) to the host. Following error is the difference between motor
desired and measured position at any instant. When the motor is open-loop (killed or
enabled), following error does not exist and PMAC reports a value of 0.
F
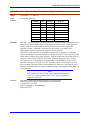
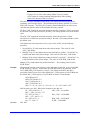
; Ask for following error of addressed motor
12
; PMAC responds
#3F
; Ask for following error of Motor 3
-6.7
; PMAC responds
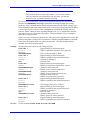
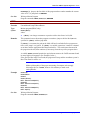
Following Error (Servo Features)
I-variables Ix11, Ix12, Ix67
On-line commands <CTRL-F>, P, V
Suggested M-variable definitions Mx61, Mx62
Memory map registers D:$0028, D:$002C, etc.; D:$0840, etc.
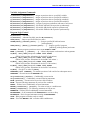
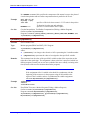
FRAX
Function
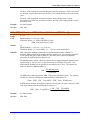
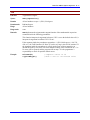
Specify the coordinate system’s feedrate axes.
Scope
Coordinate-system specific
Syntax
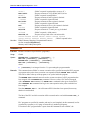
FRAX
FRAX({axis}[,{axis}...])
where:
•
{axis} (optional) is a character (X, Y, Z, A, B, C, U, V, W) specifying which axis is to
be used in the vector feedrate calculations
Note:
No spaces are permitted in this command.
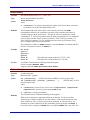
Remarks
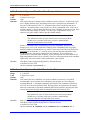
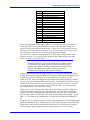
This command specifies which axes are to be involved in the vector-feedrate (velocity)
calculations for upcoming feedrate-specified (F) moves. PMAC calculates the time for these
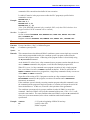
moves as the vector distance (square root of the sum of the squares of the axis distances) of
all the feedrate axes divided by the feedrate. Any non-feedrate axes commanded on the same
line will complete in the same amount of time, moving at whatever speed is necessary to
cover the distance in that time.
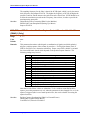
Vector feedrate has obvious geometrical meaning only in a Cartesian system, for which it
results in constant tool speed regardless of direction, but it is possible to specify for nonCartesian systems, and for more than three axes.
Note:
If only non-feedrate axes are commanded to move in a feedratespecified move, PMAC will consider the axis or axes commanded to
be feedrate axes for that move. However, the units of these axes may
be completely different from those of the vector feedrate axes (e.g.
degrees instead of mm), so the speed may not be what is desired.
3-66
PMAC On-Line Command Specification