1
Example:
After having run the welding tests, the result was that the usable life of the electrodes = 2000 welding
spots. Another fact that ensued was that the required current for new electrodes = 15 kA, whereas after
2000 welding spots the diameter increase of the electrodes requires a current of 19 kA.
Therefore calculate the change in percent as follows:
Change % =
endcurrent − initialcur rent
19 − 15
× 100 =
× 100 = 26%
initialcur rent
15
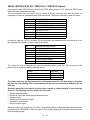
Consequently the following parameters are set in the "Stepper" menu:
PARAMETER
DESCRIPTION
VALUE
STEPS INCREM
Number of segments for stepper function
SPOTS 1
First segment spots number
2000
INCREMENT1
First segment increment percent
26%
1
The welding program should be adjusted for carrying out the first welding spot followed by the
adjustment that permits to obtain the required current with the starting electrode diameter: 15 kA.
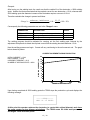
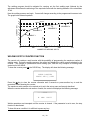
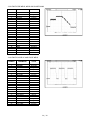
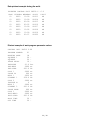
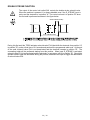
Now the welding process can begin. Current will vary conforming to the set increment rule. The graph
below shows its pattern.
CURRENT INCREMENT DURING PRODUCTION
20
WELDING CURRENT (kA
INITIAL CURRENT = 15 kA
END CURRENT = 19 kA
INCREMENT PERCENT = 26 %
NUMBER OF WELDING SPOTS = 2000
18
16
14
12
10
8
6
4
2
0
0
500
1000
1500
NUMBER OF WELDING SPOTS
2000
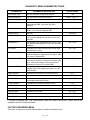
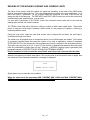
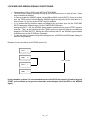
Upon having completed all 2000 welding spots the TE600 stops the production cycle and displays the
following message:
------STOP-----MAX. N. of SPOTS
At this point the operator replaces the electrodes (or resets their original diameter) and clears
the spots counter to clear stepper calculations. The TE600 resets the initial work parameters
and begins a new increment phase.
15 / 42